Dongguan Hui Lian Intelligent Warehouse Equipment Co., Ltd. is a professional warehouse storage equipment manufacturer specializing in the design, production, and supply of high-quality storage racks and intelligent warehouse solutions. Established in 2016, the company has developed extensive expertise in the warehousing equipment industry, providing reliable storage solutions for customers worldwide.
With a factory area of approximately 18,500㎡, Hui Lian Intelligent Warehouse Equipment integrates advanced manufacturing technology, professional engineering capabilities, and strict quality management systems. The company achieves an annual export revenue of around US$18 million and has accumulated 8 years of export experience and 15 years of industry experience, serving customers across multiple international markets.
18,500㎡
Advanced Factory Area
15+
Years Industry Experience
56
Professional QC Inspectors
850+
Global Supply Partners
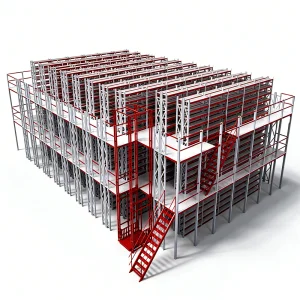
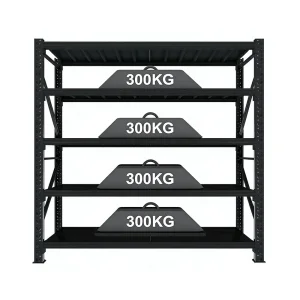
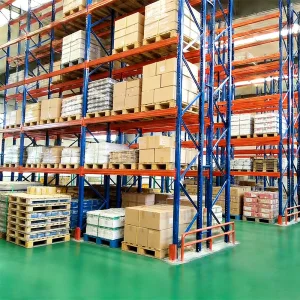
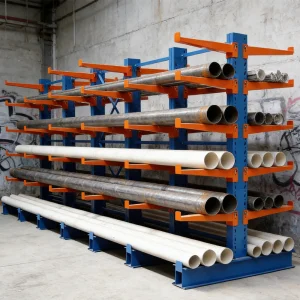
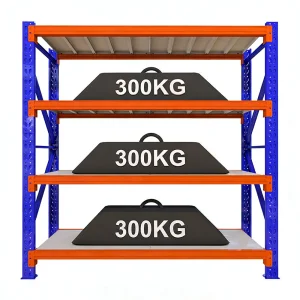
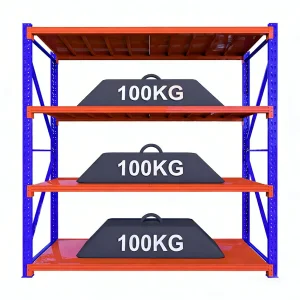
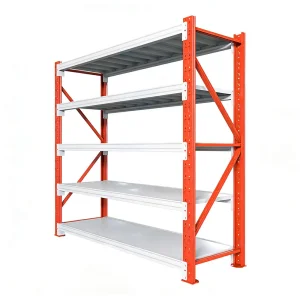
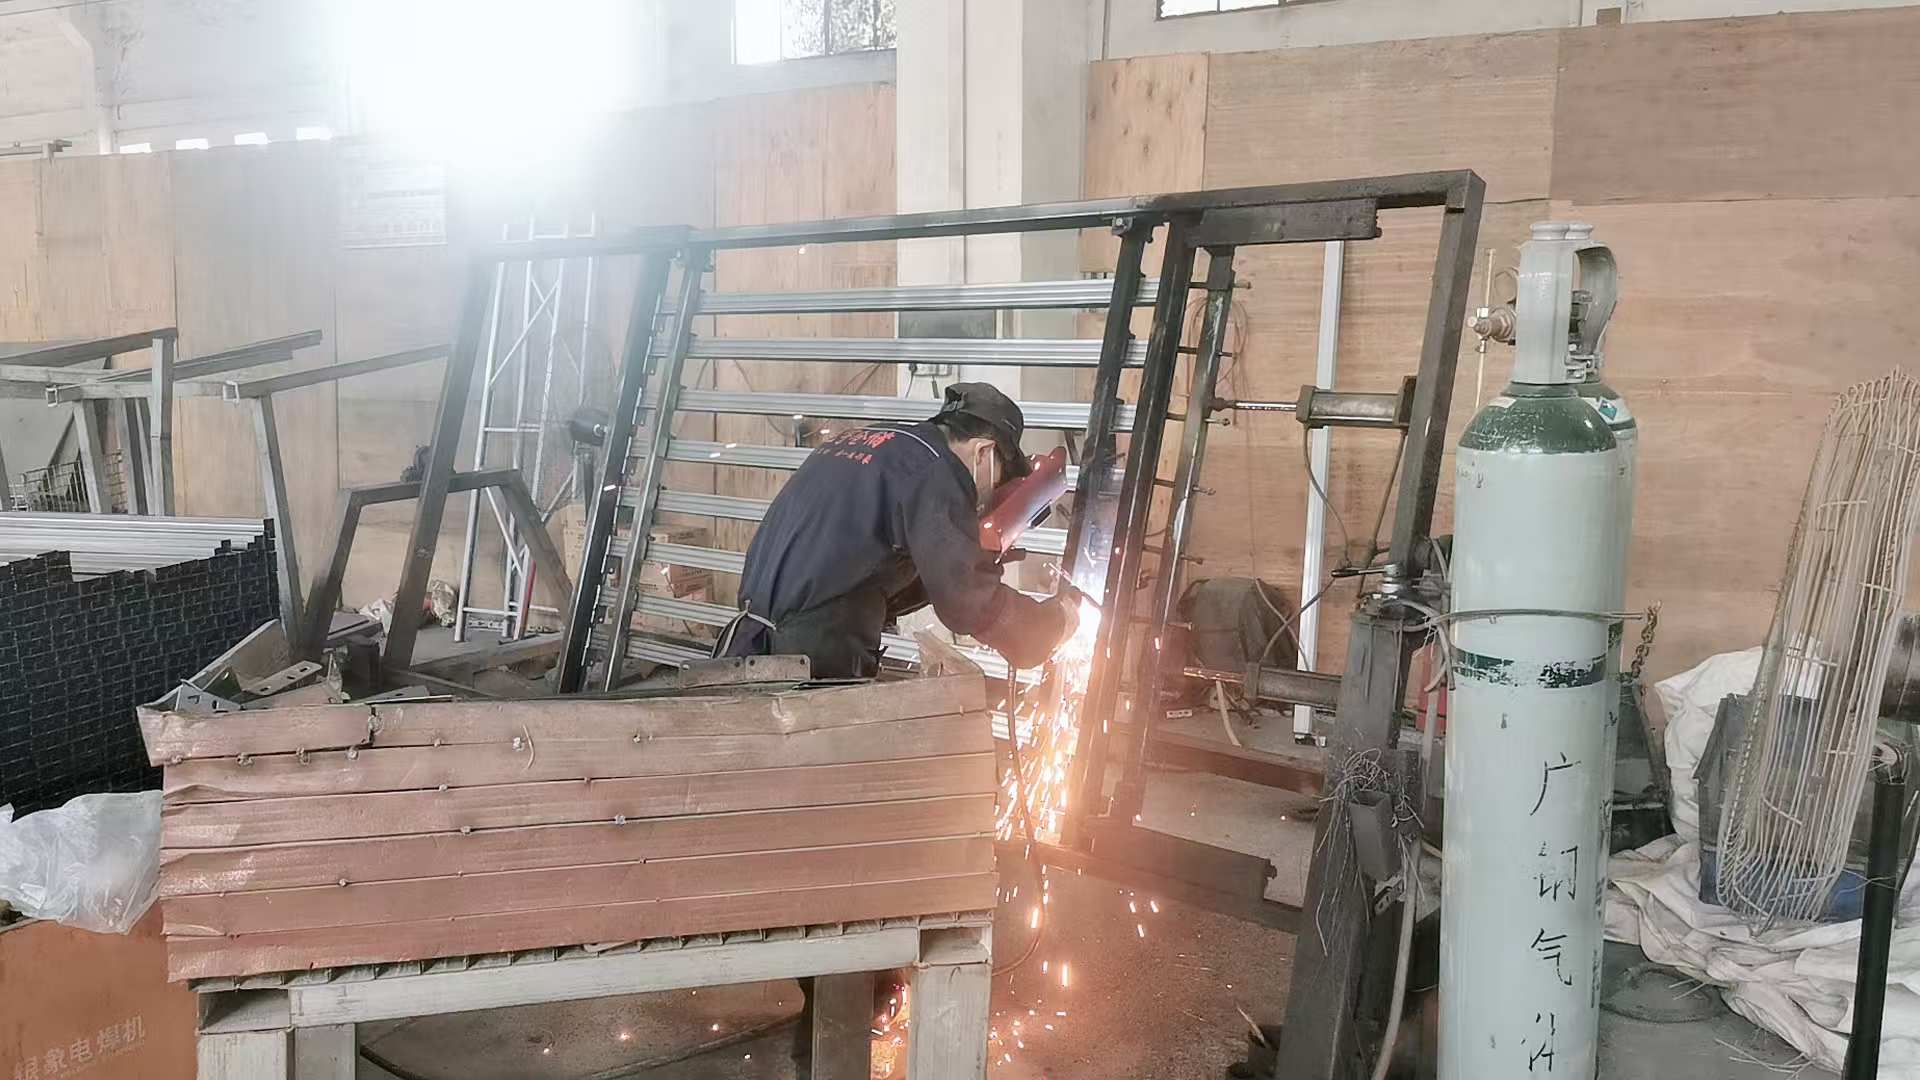
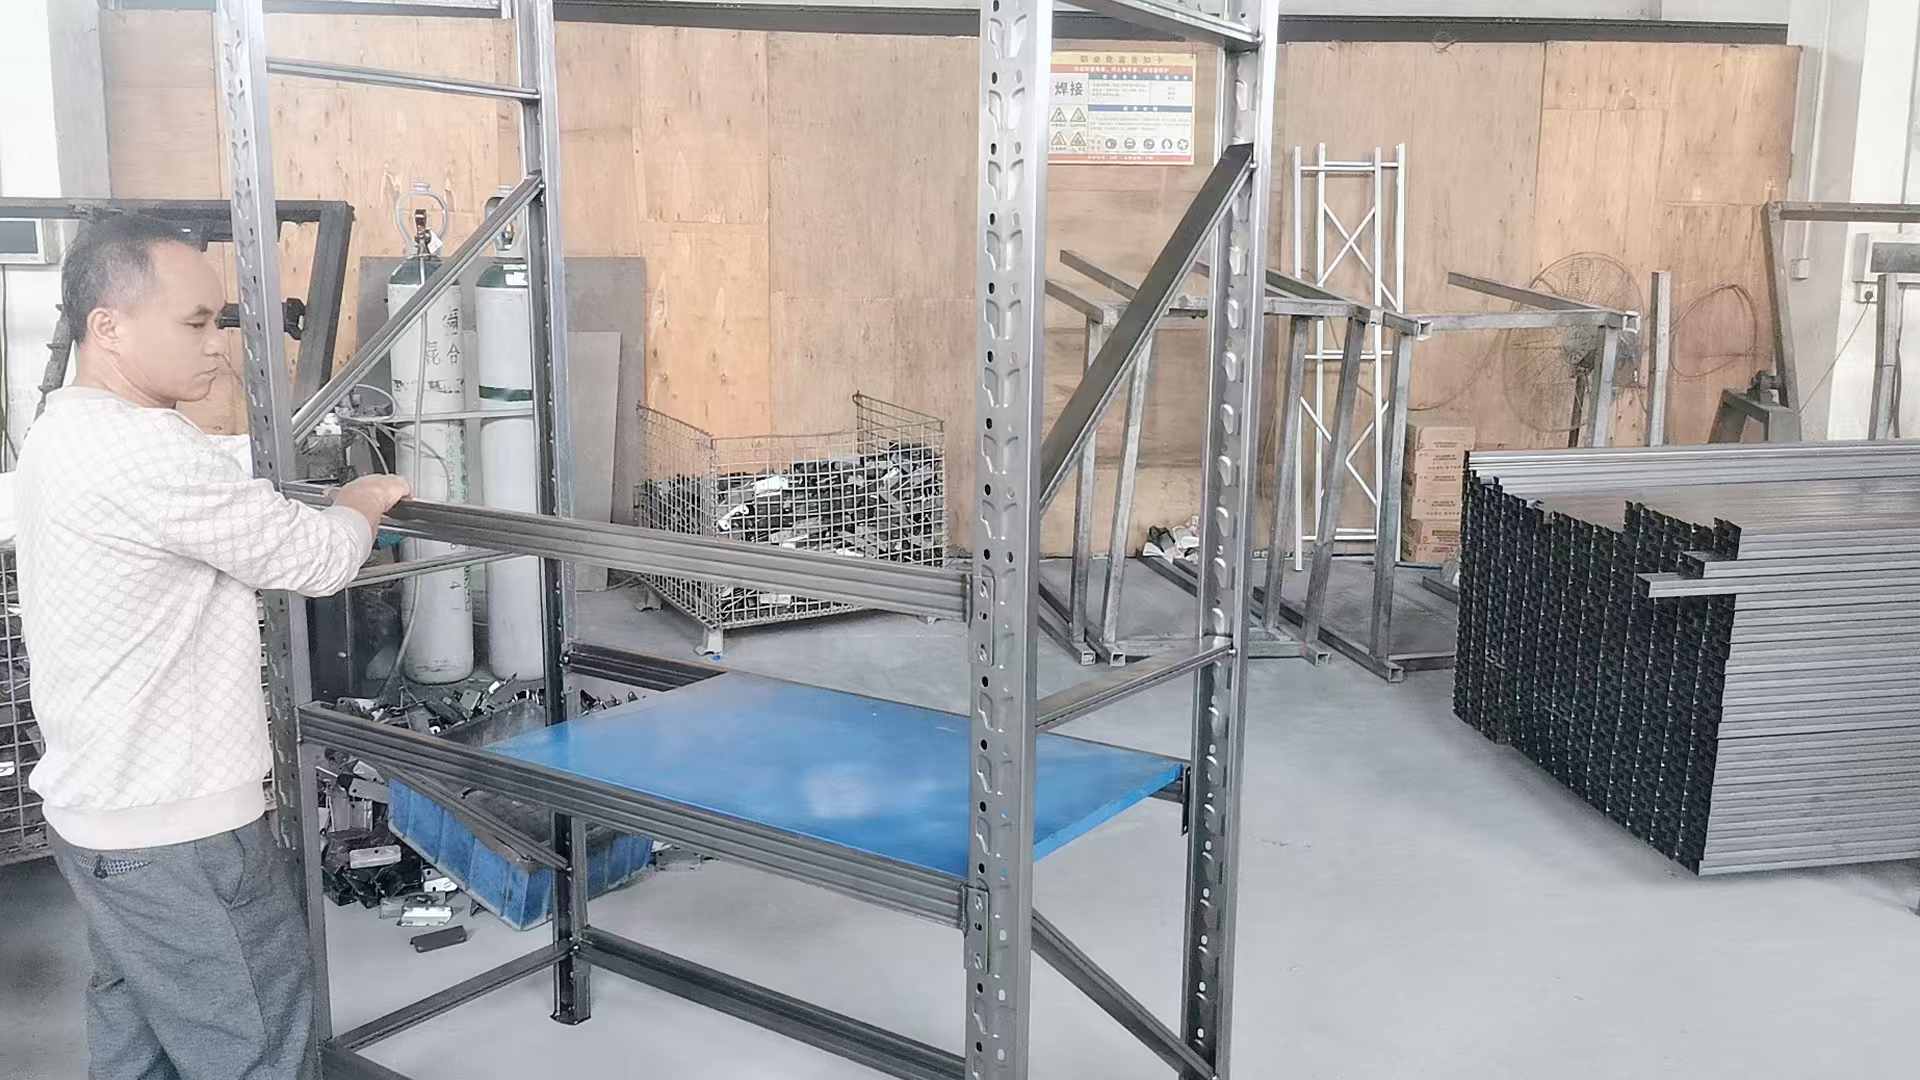
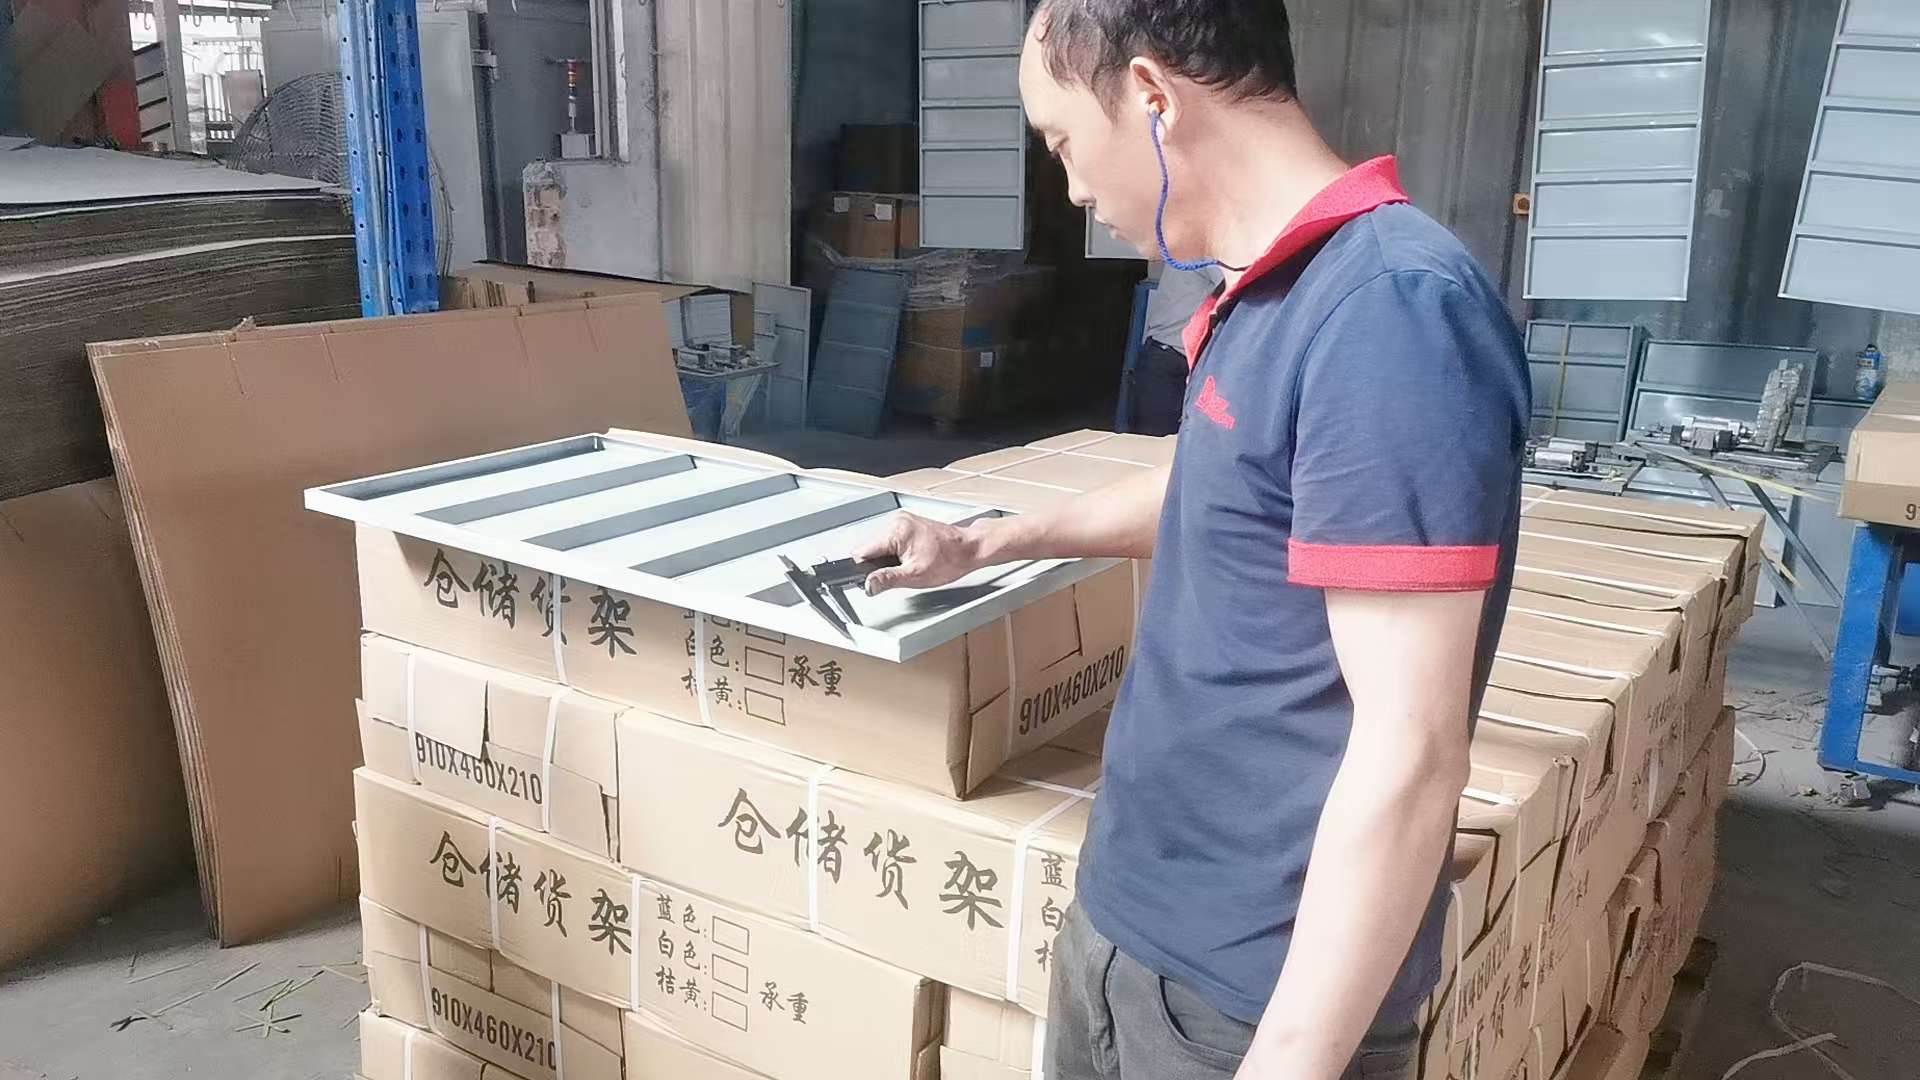
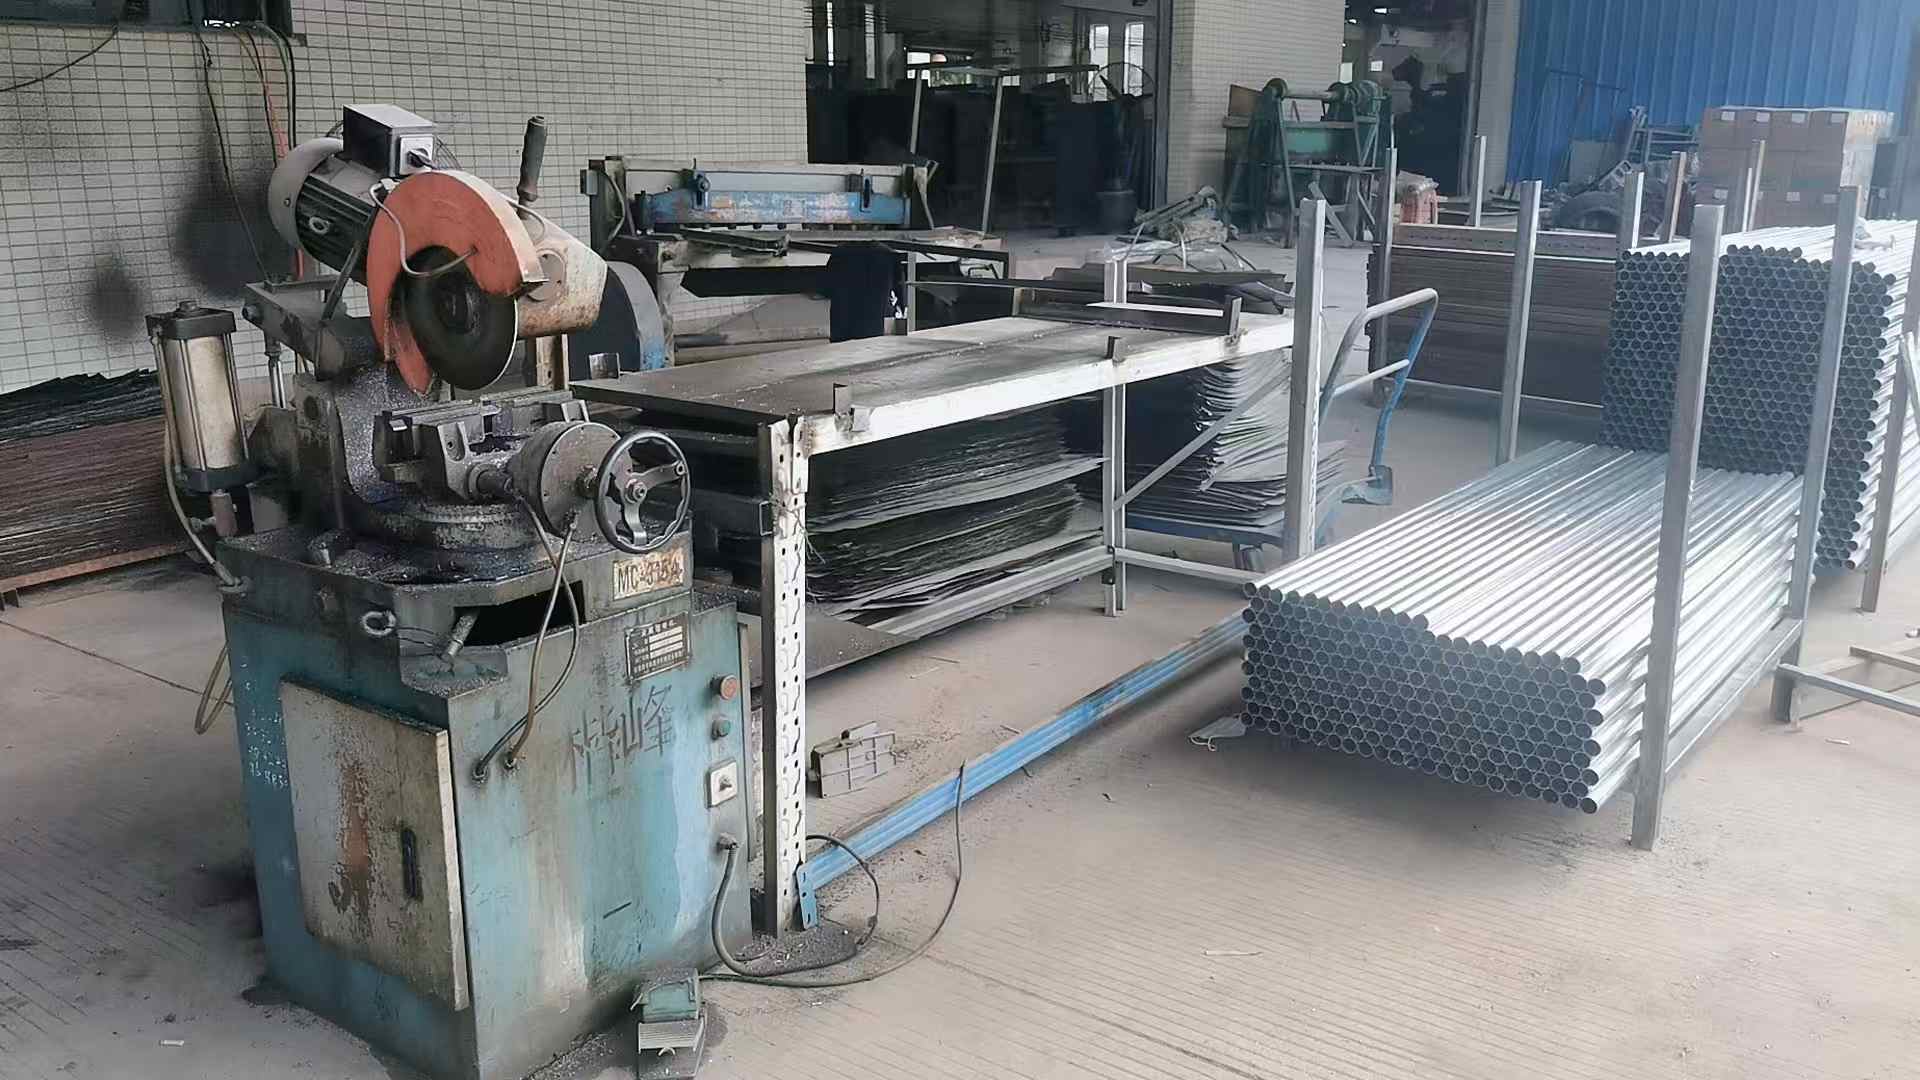
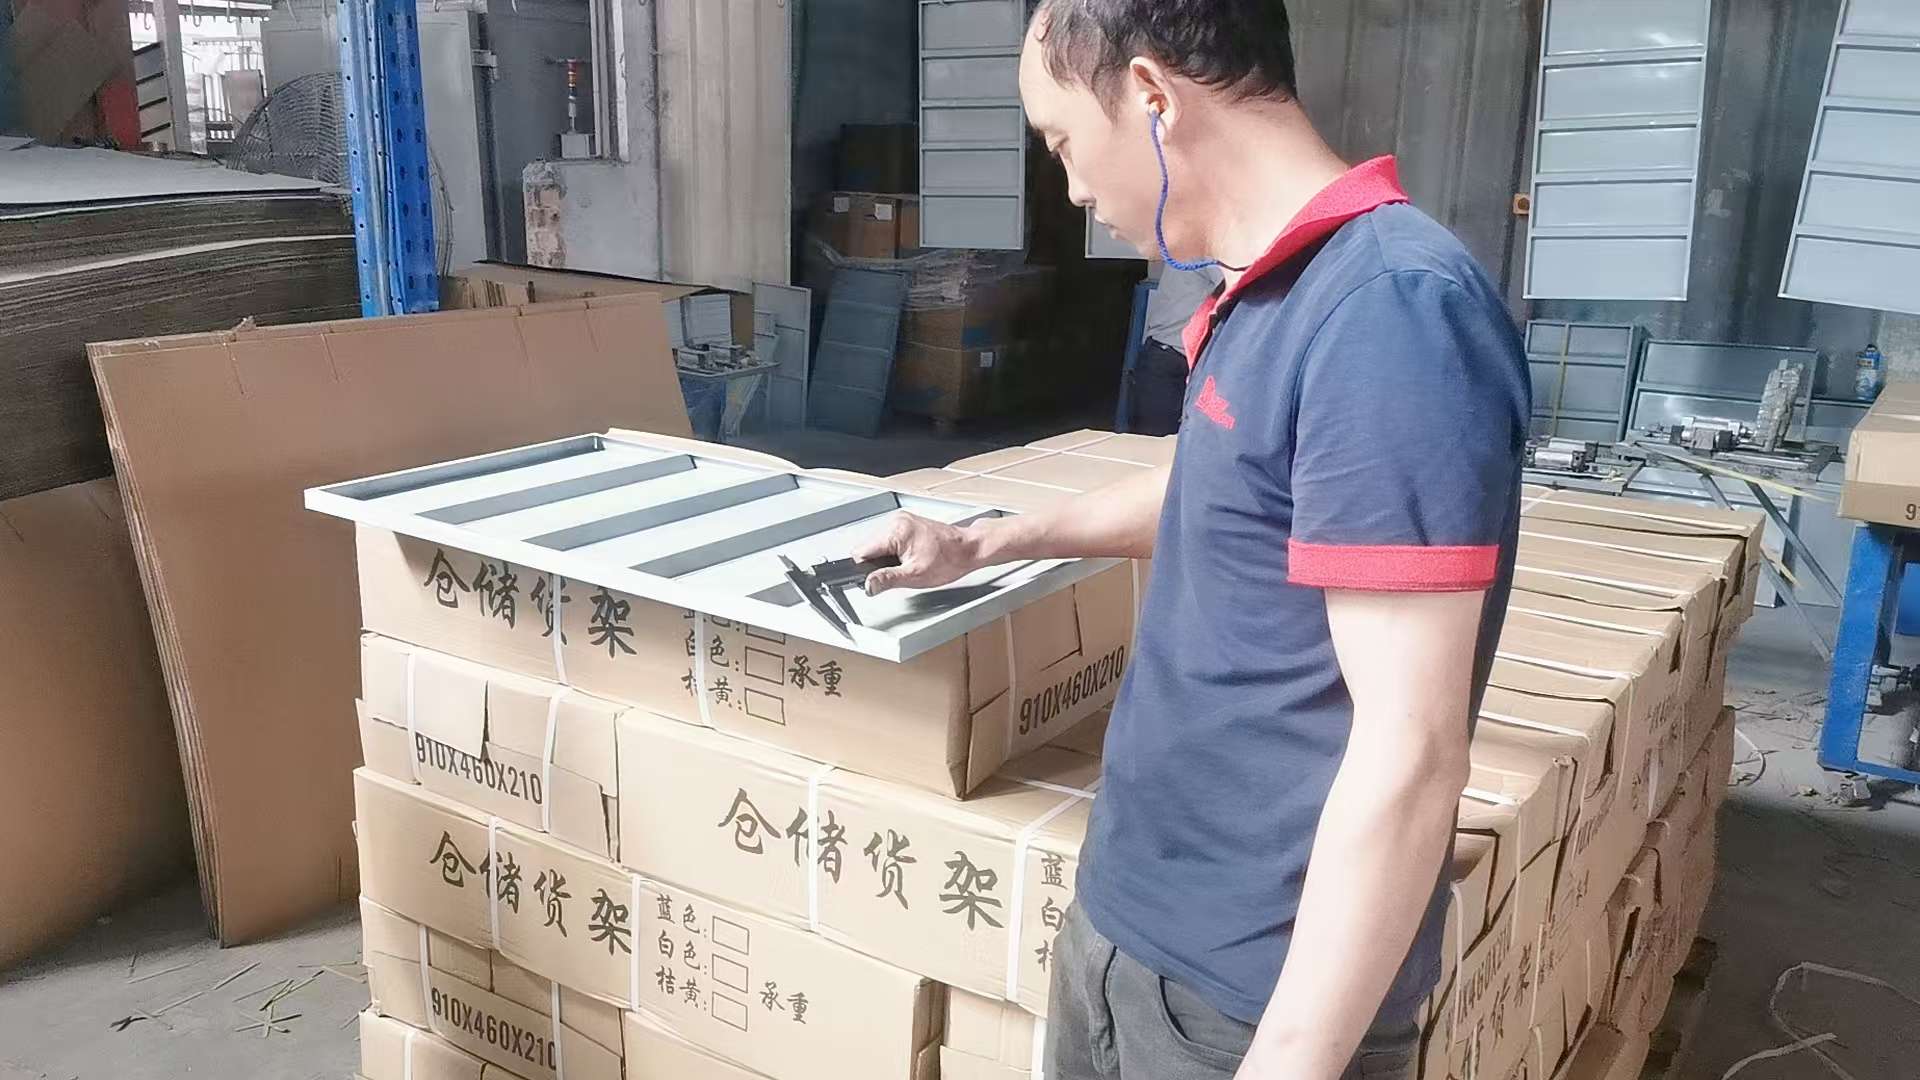
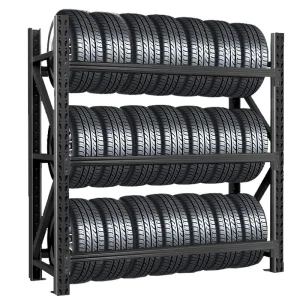
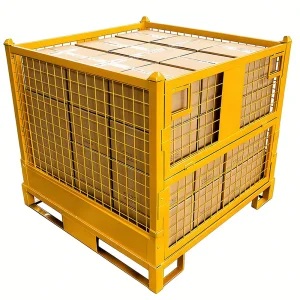
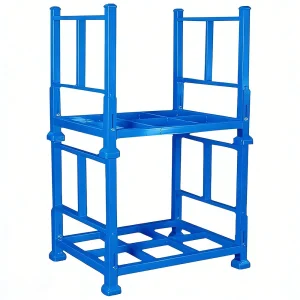
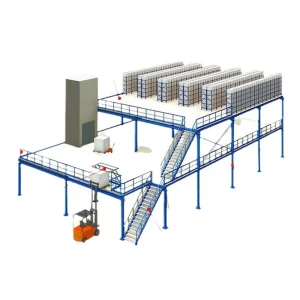
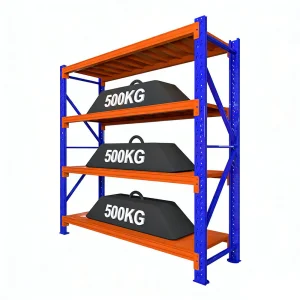
Our product range includes pallet racks, heavy-duty storage racks, automated warehouse racks, mezzanine floors, cantilever racks, warehouse shelving systems, and customized storage solutions. All products undergo strict quality inspection processes, including raw material inspection, welding quality checks, dimensional accuracy testing, load-bearing tests, surface treatment inspection, and finished product evaluation to ensure safety, durability, and performance.
The company has a dedicated quality control team of 56 professional inspectors responsible for monitoring every stage of production, from material selection to final shipment. Hui Lian follows international quality standards and applies advanced inspection equipment such as laser measurement tools, load testing equipment, coating thickness gauges, and automated inspection systems.
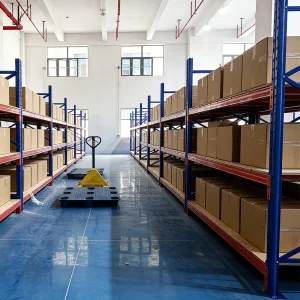
With a strong trade background combining manufacturing, international export, OEM/ODM cooperation, and global supply chain management, Hui Lian has established stable partnerships with customers in North America, Europe, Southeast Asia, the Middle East, Australia, and South America. The company serves a wide range of clients, including logistics companies, e-commerce warehouses, manufacturing enterprises, retail distributors, third-party logistics providers, and large-scale warehouse operators.
Hui Lian Intelligent Warehouse Equipment works closely with more than 850 supply chain partners, ensuring efficient material sourcing, stable production capacity, and competitive delivery performance. The company provides comprehensive customization services, including custom dimensions, structural design, load capacity solutions, surface treatments, colors, and complete warehouse planning services.
Driven by continuous innovation, Hui Lian maintains a strong research and development capability with 126 professional R&D engineers focused on improving warehouse efficiency and developing advanced storage solutions. In the past year, the company launched 320 new products to meet evolving market demands and provide customers with smarter and more flexible warehouse systems.
Through professional manufacturing, strict quality control, and customer-focused service, Dongguan Hui Lian Intelligent Warehouse Equipment Co., Ltd. is committed to becoming a trusted global partner for intelligent warehouse equipment and storage rack solutions.
The global industrial tool storage and warehouse racking sector is undergoing a profound transformation driven by Industry 4.0 automation, smart supply chain optimization, and rigorous international safety certifications (such as CE compliance). Modern manufacturing plants, third-party logistics (3PL) providers, and automotive assembly hubs increasingly demand high-load capacity, modular adaptability, and anti-corrosion durability to maximize vertical space utilization and minimize operational downtime.
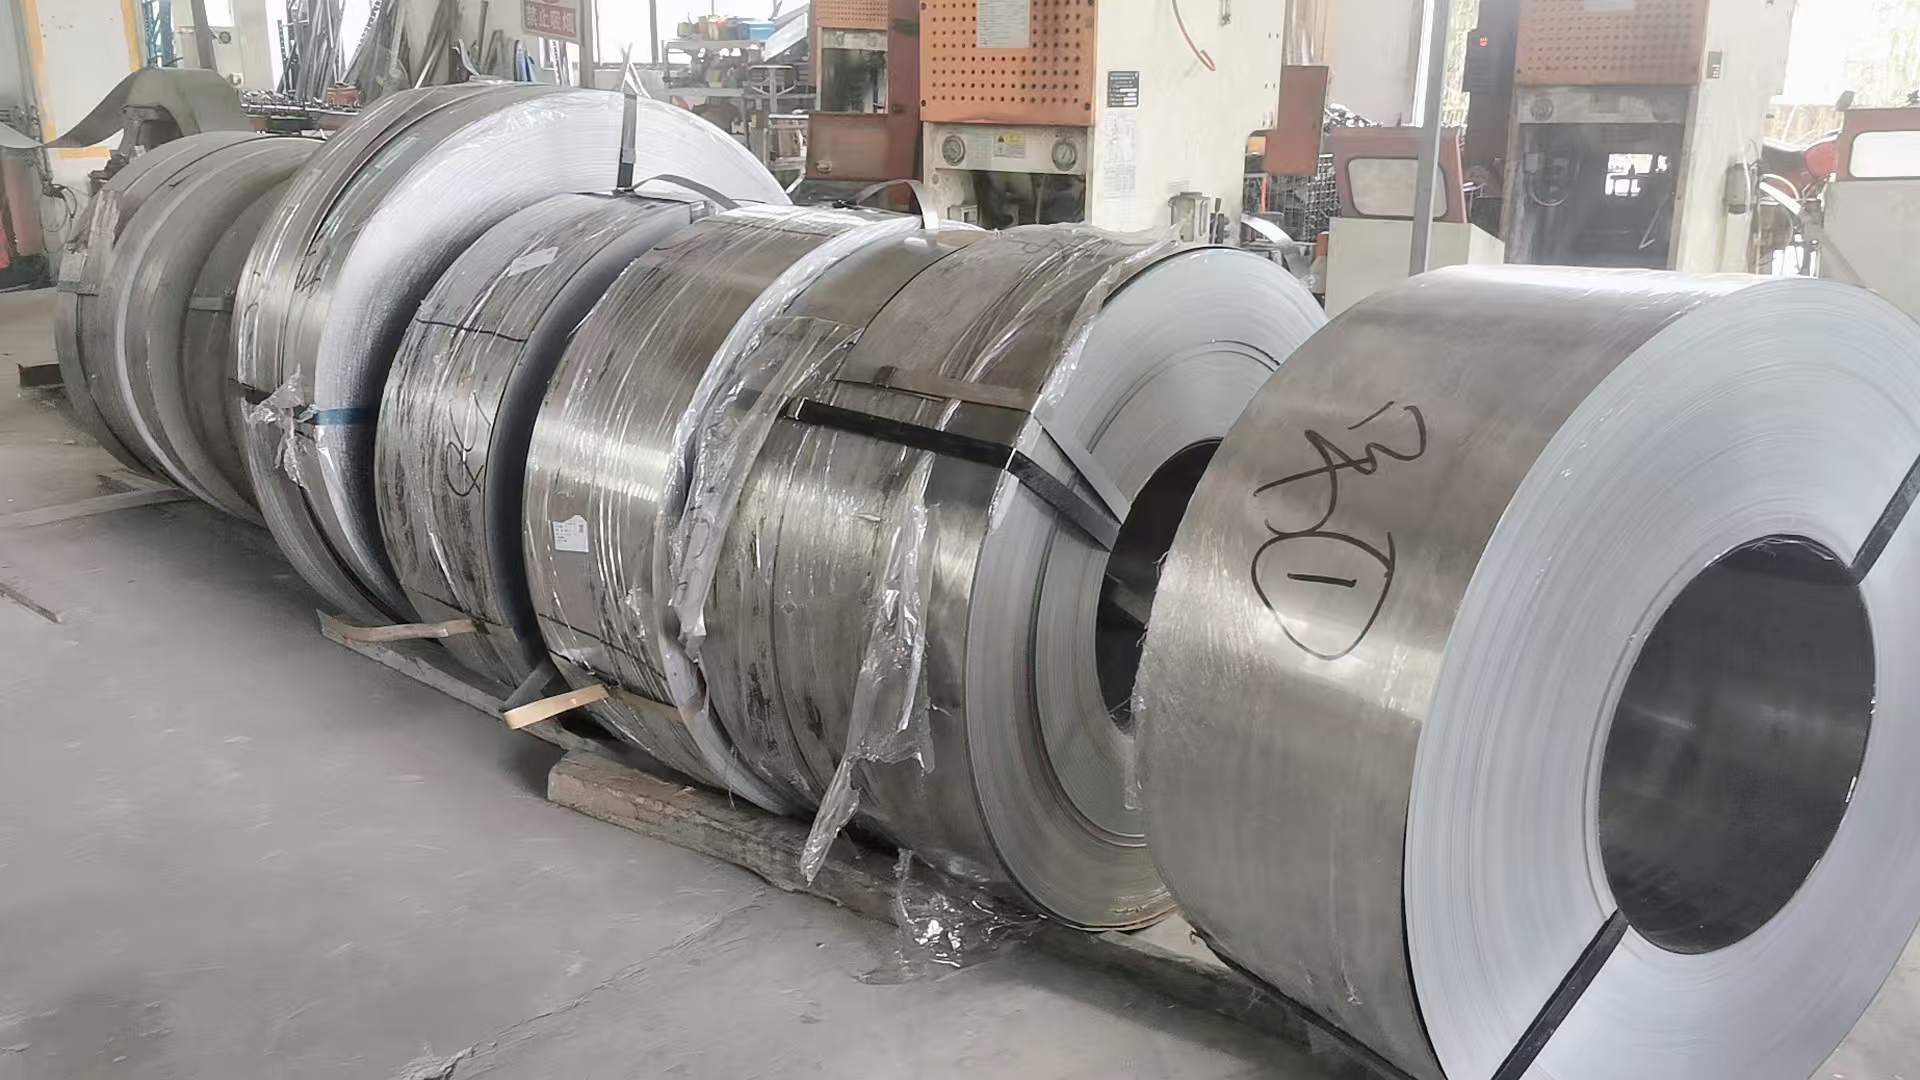
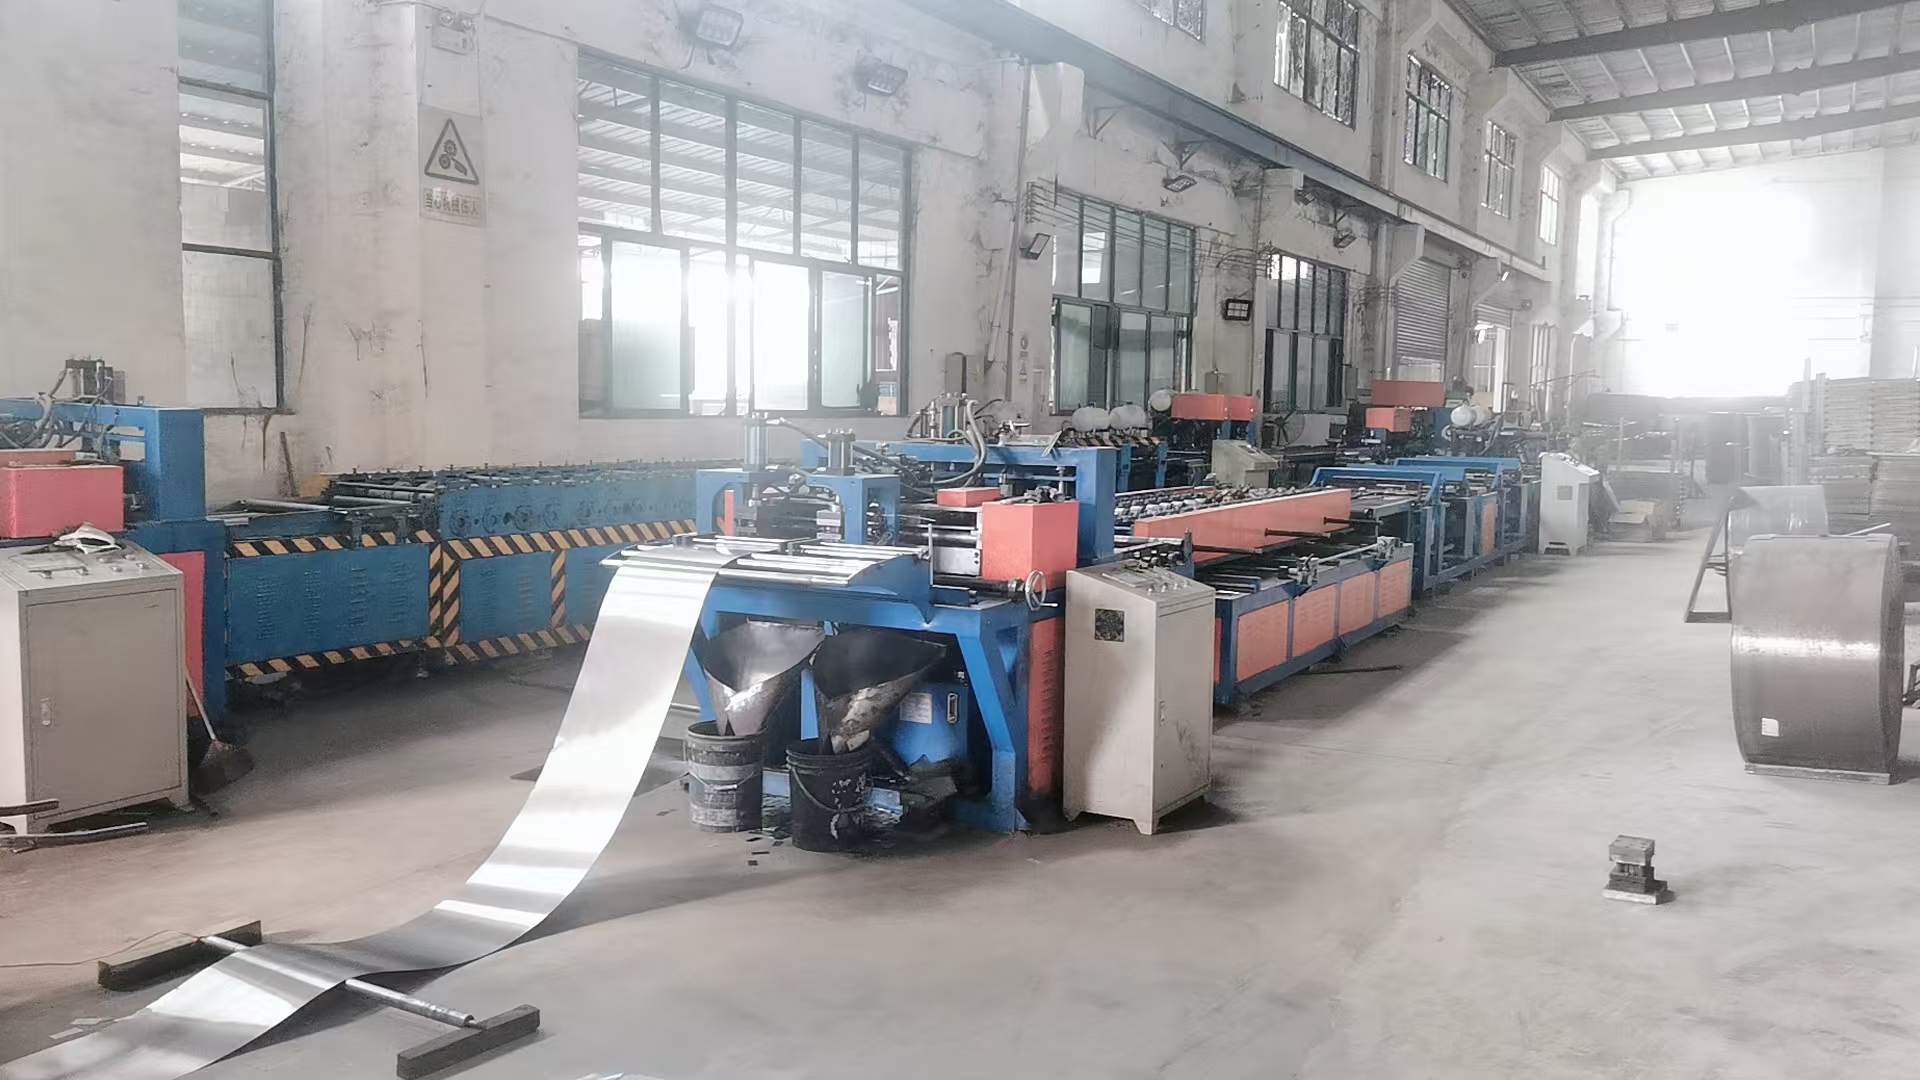
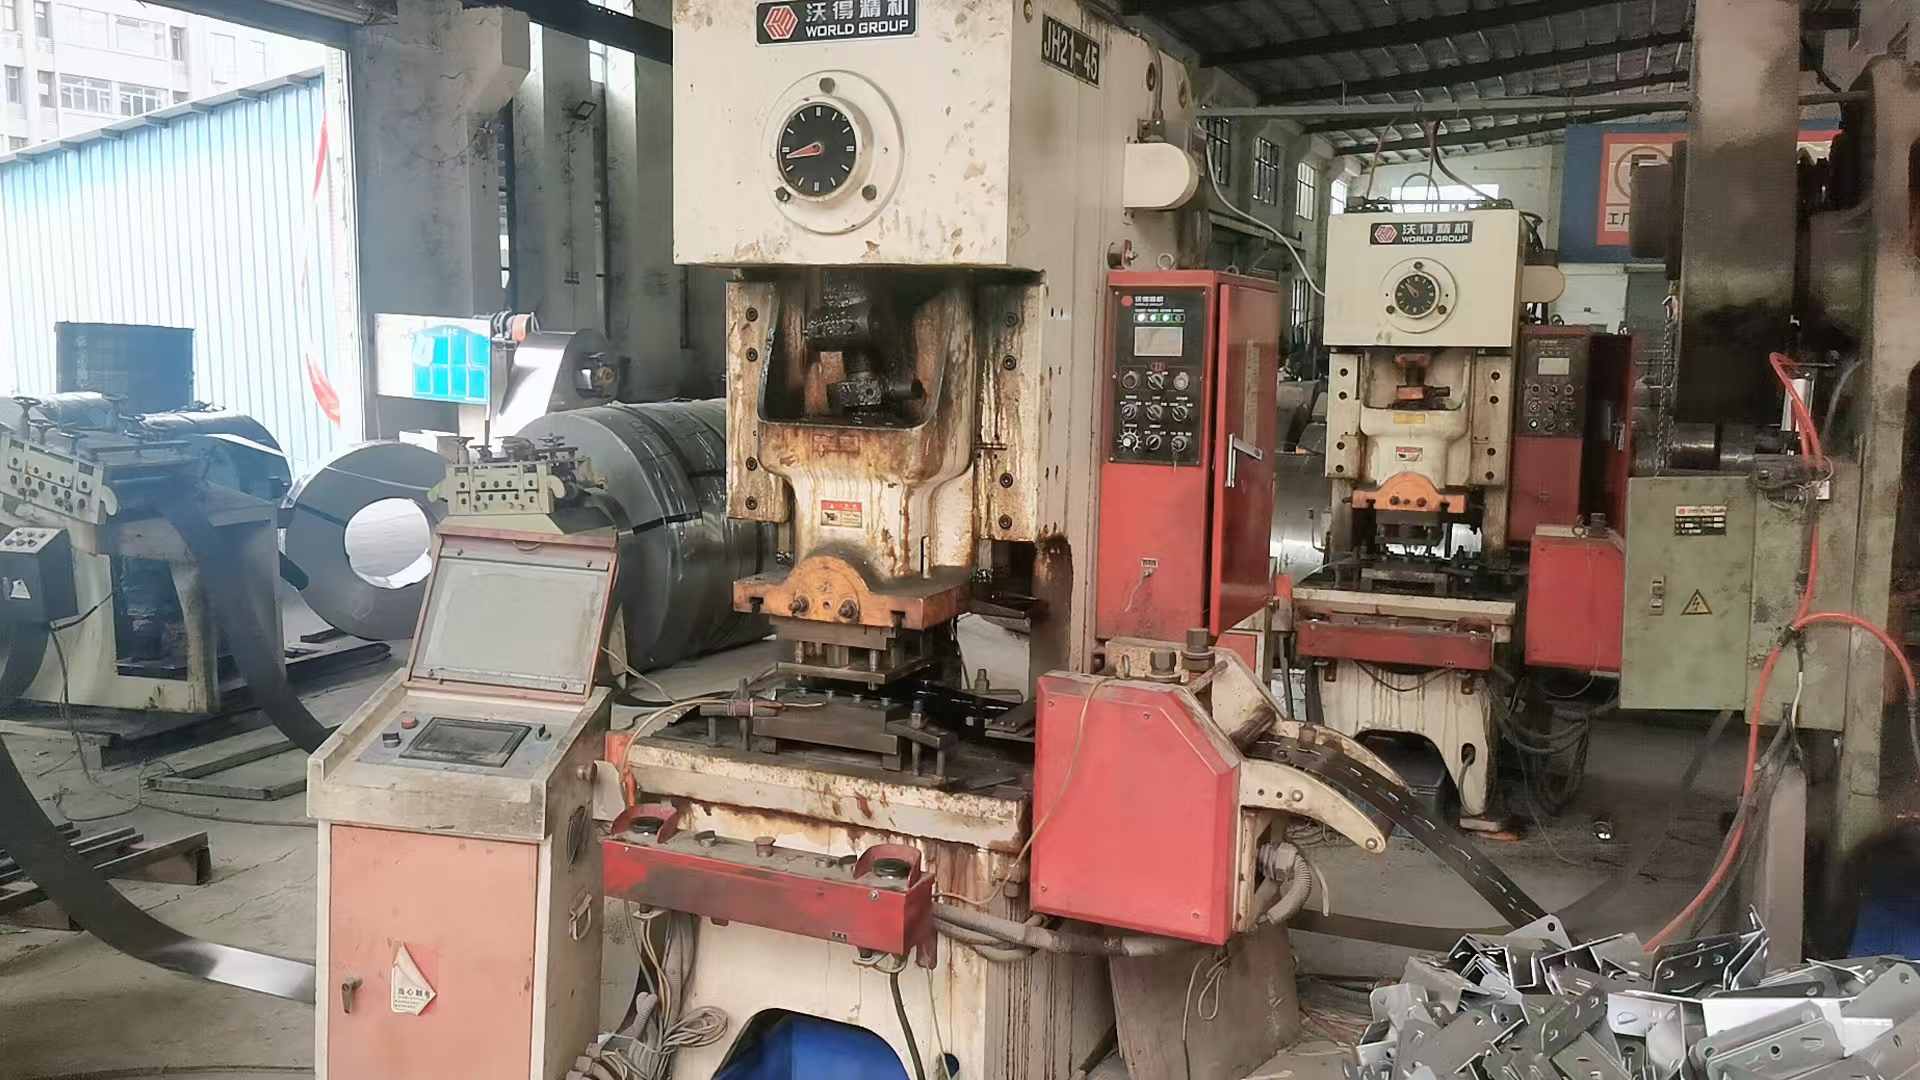
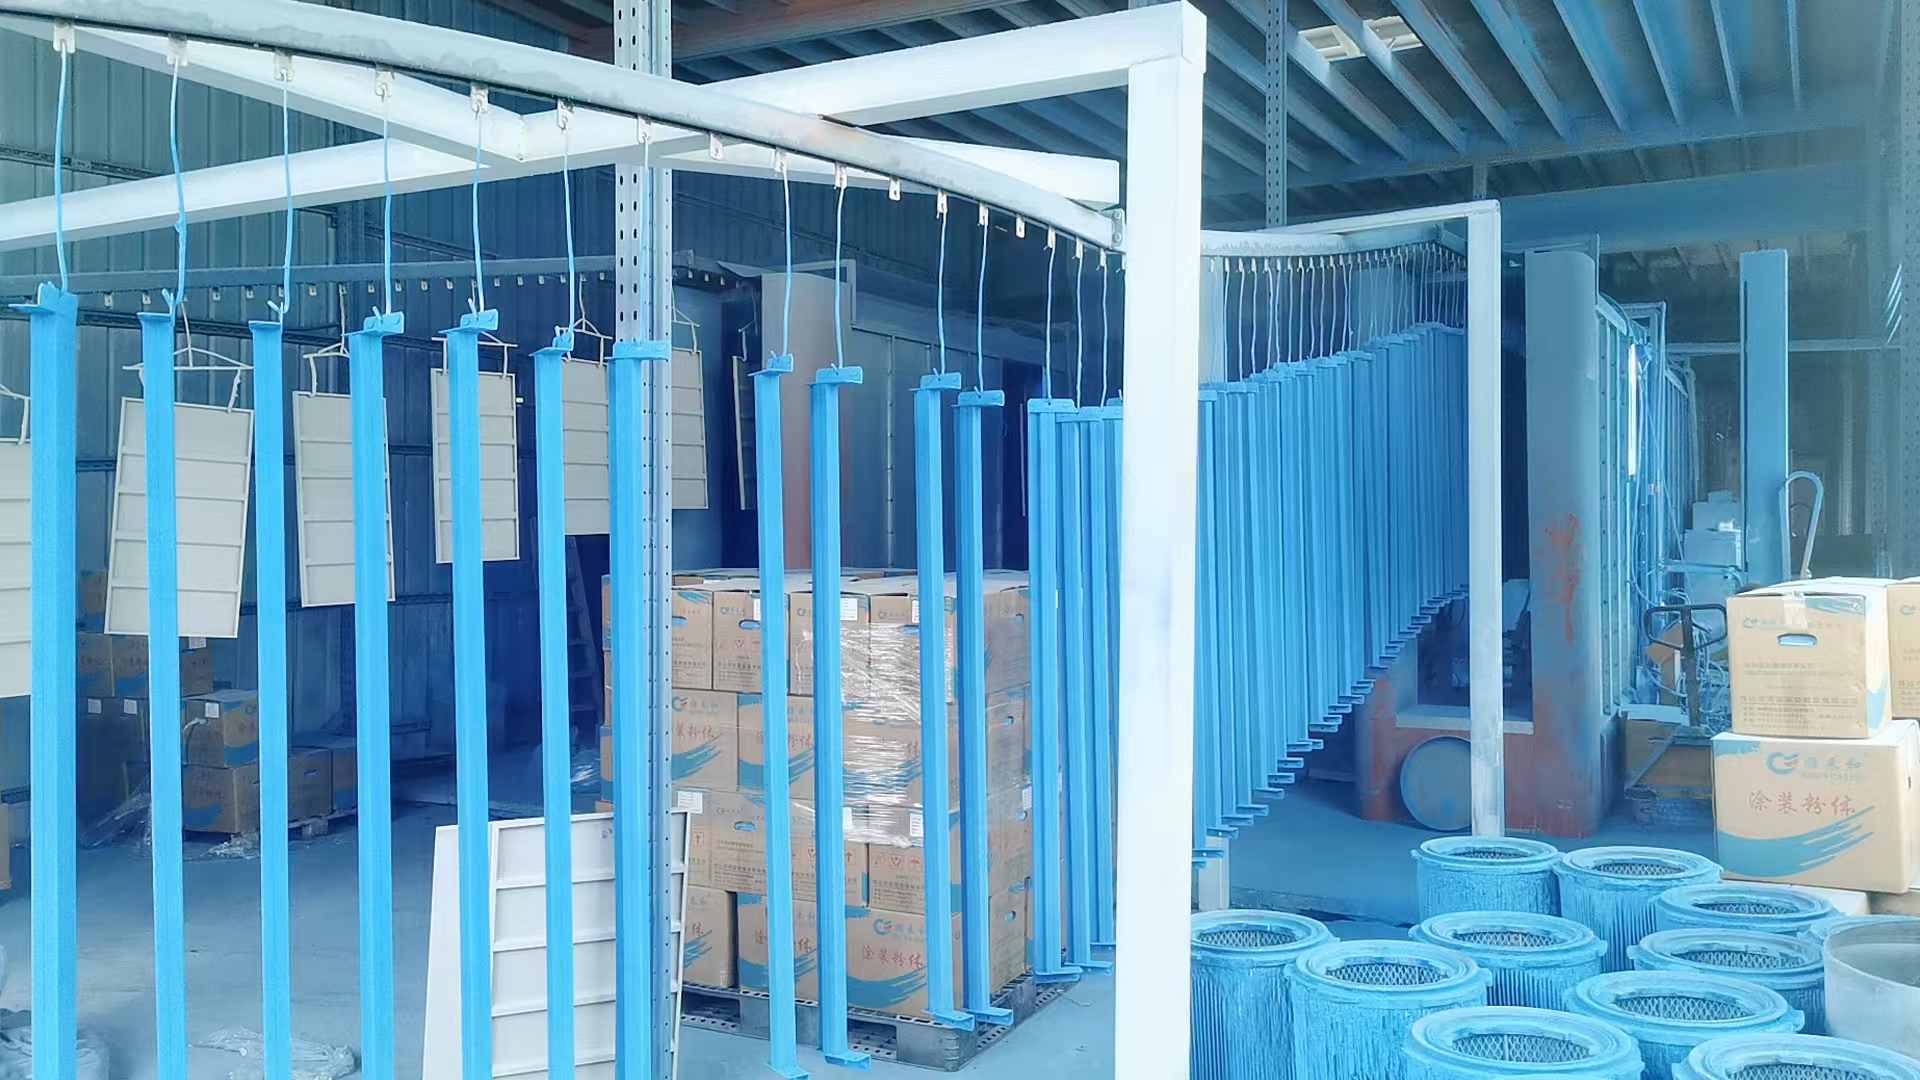
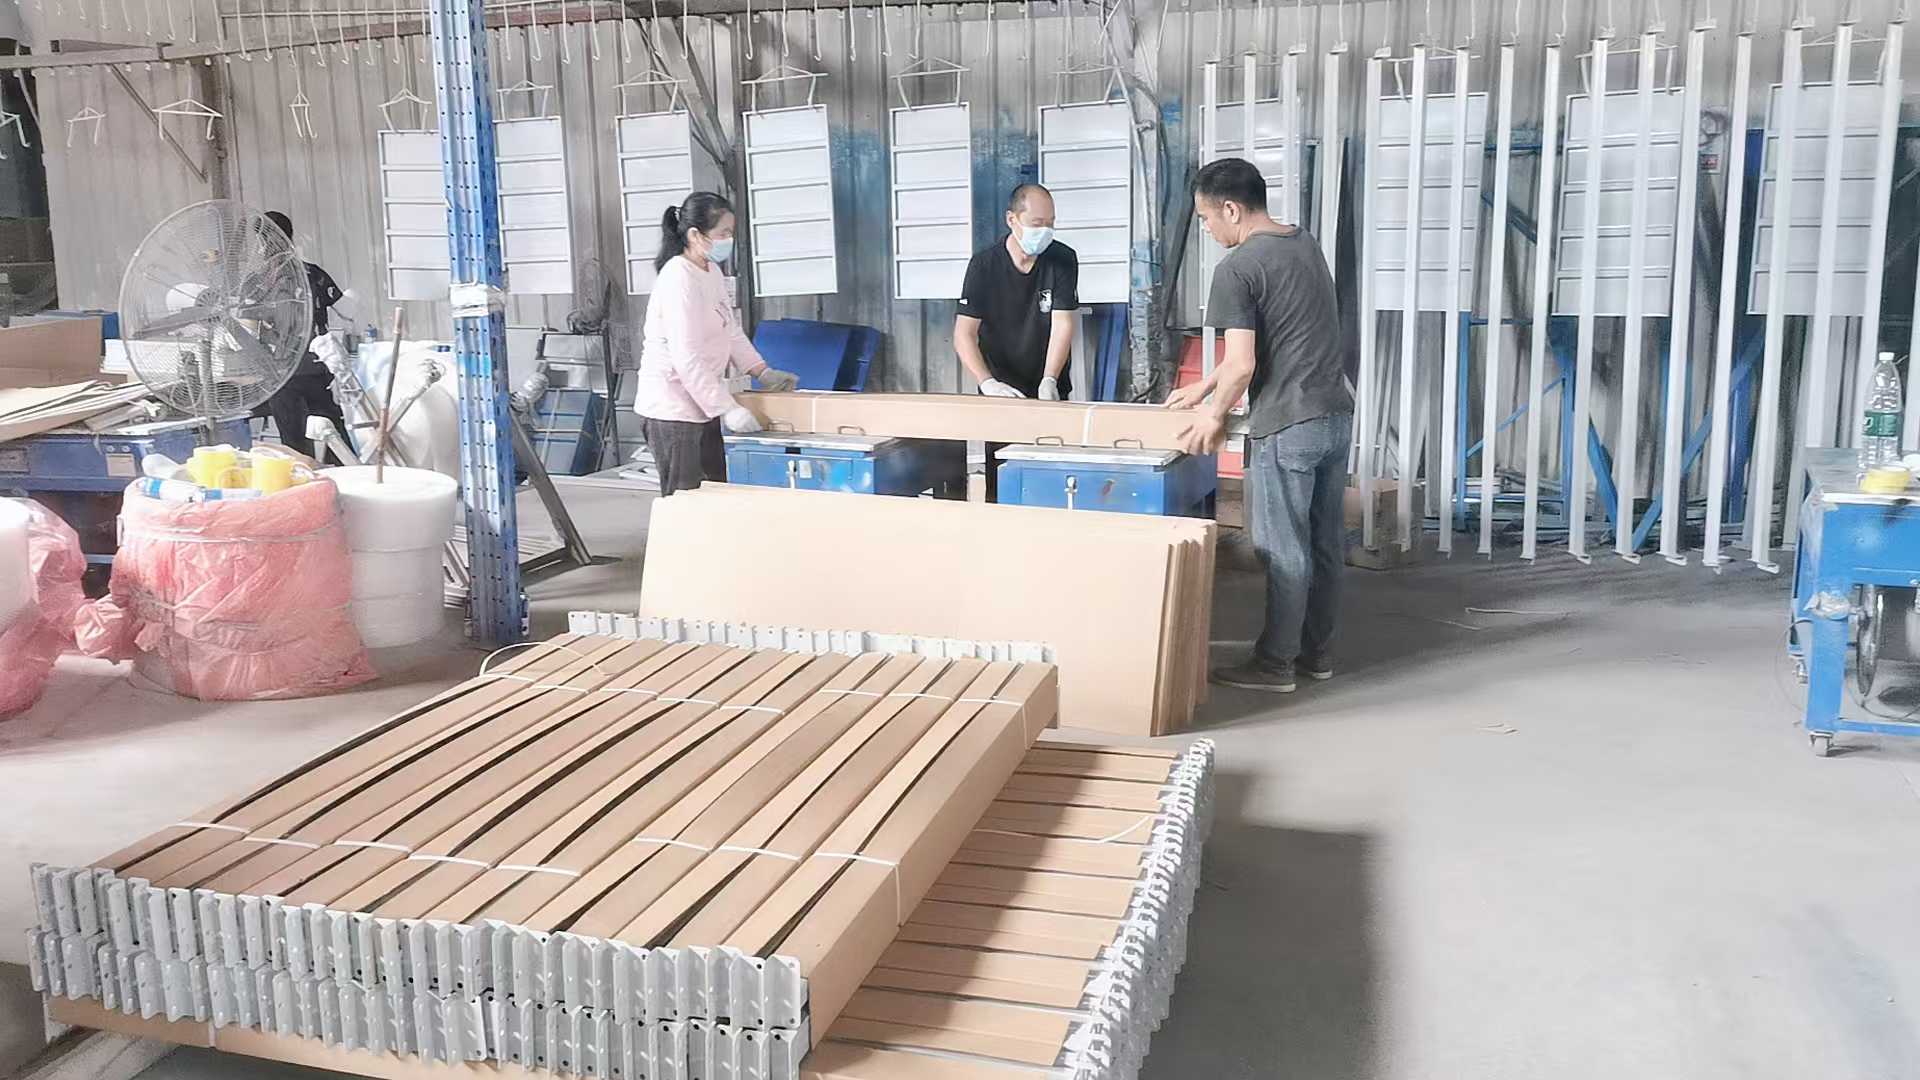
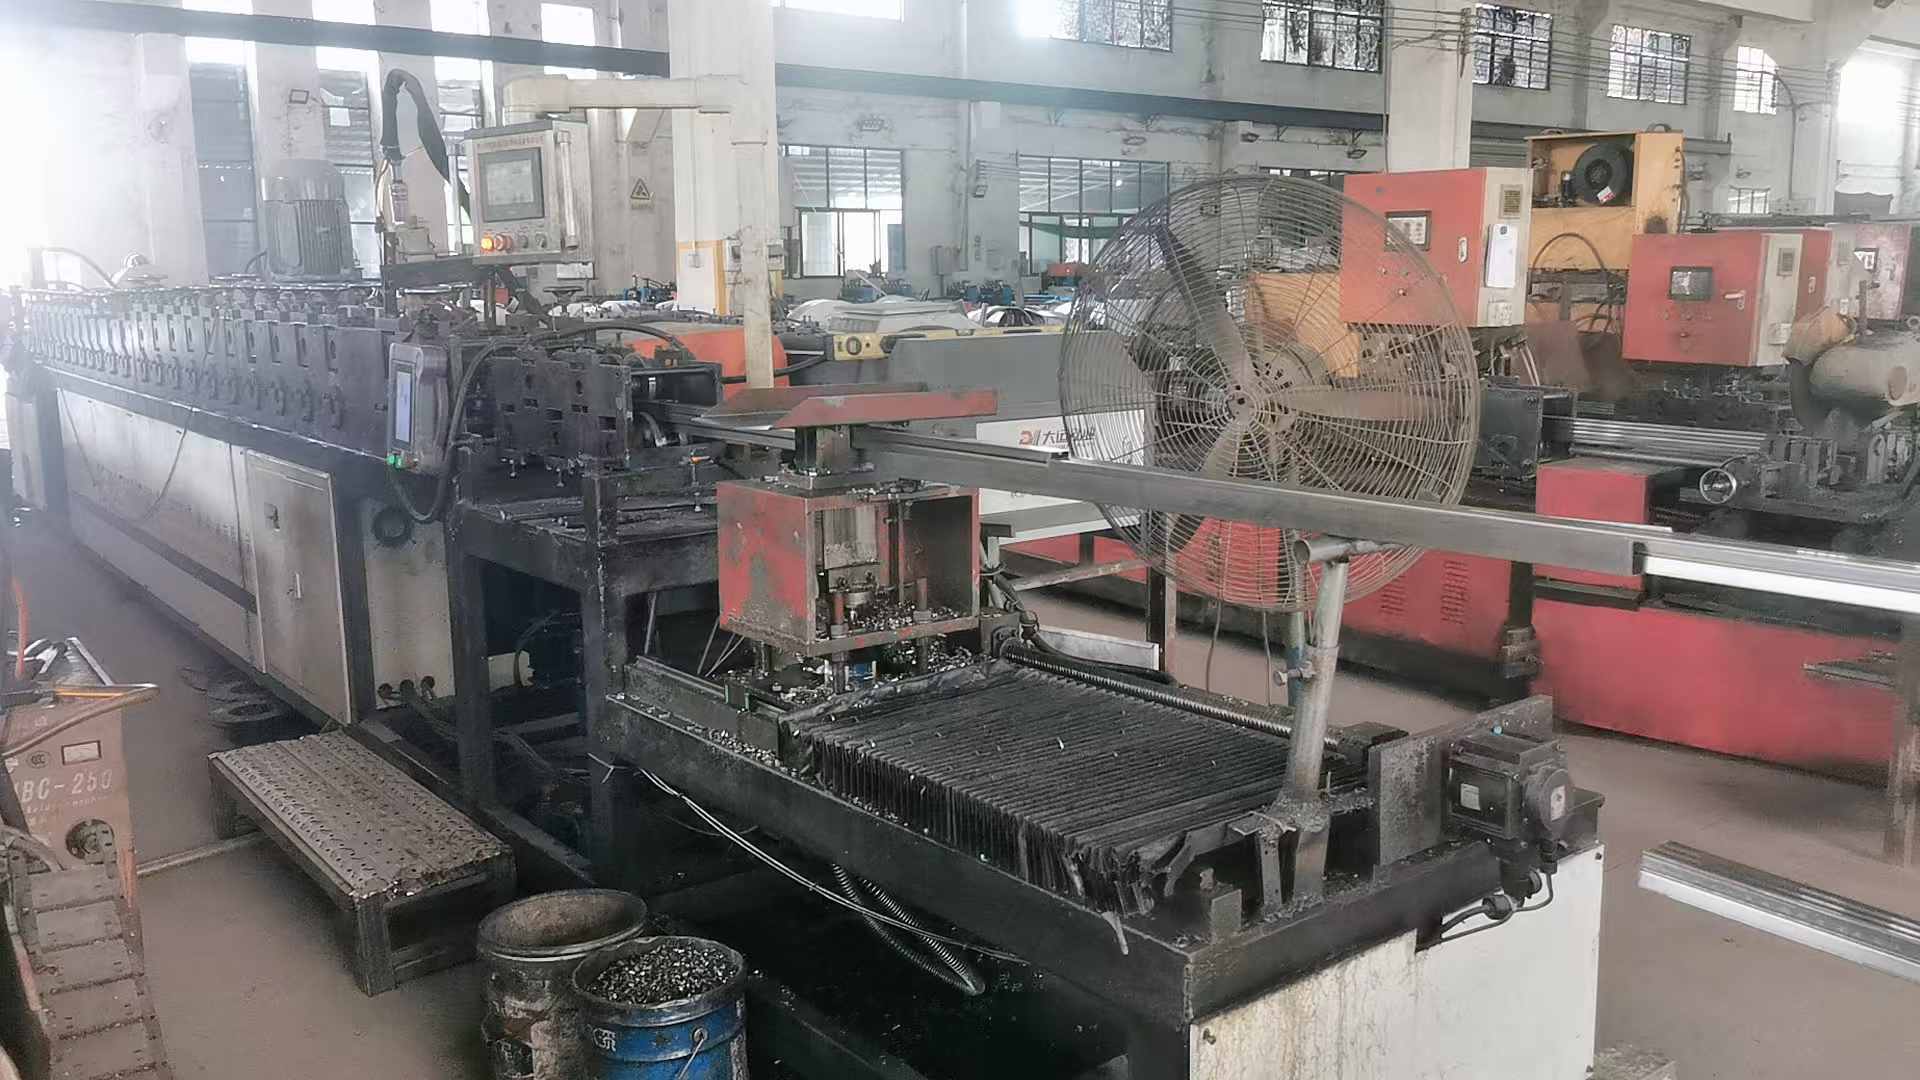
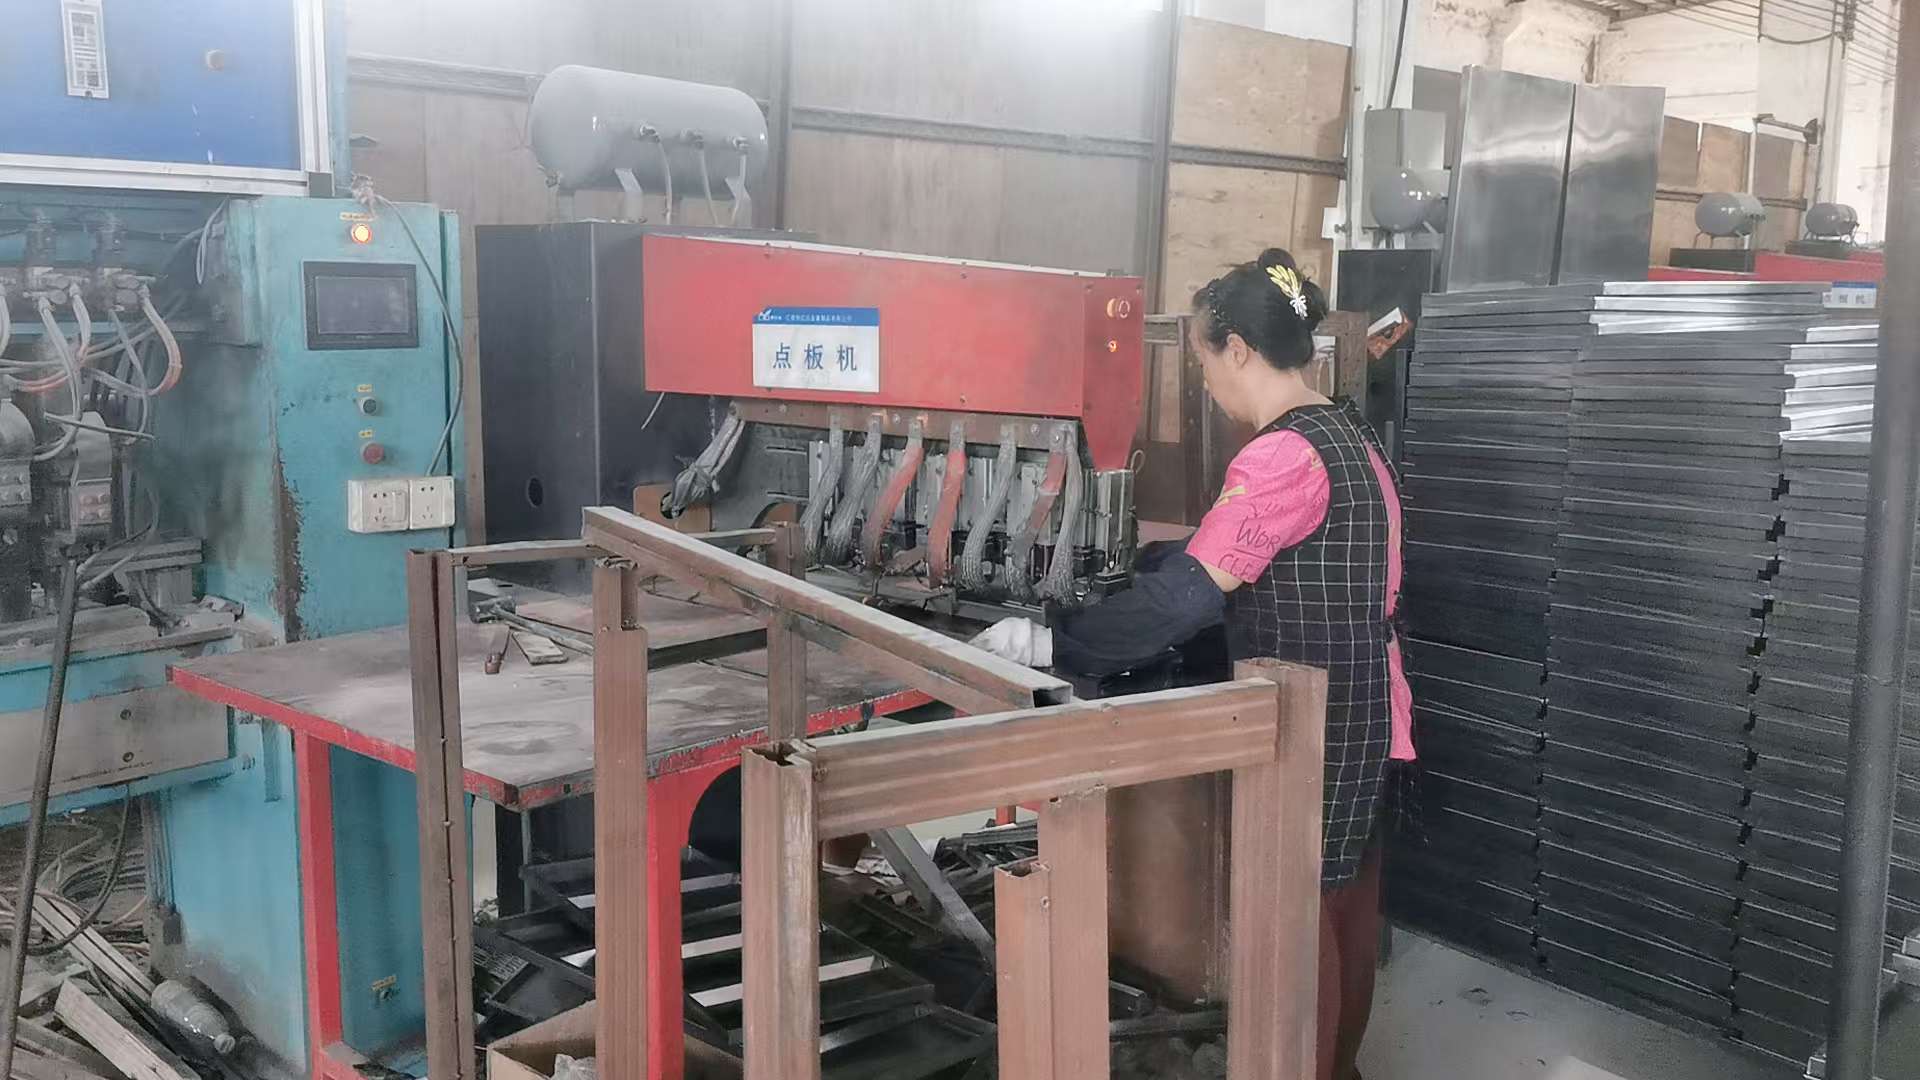
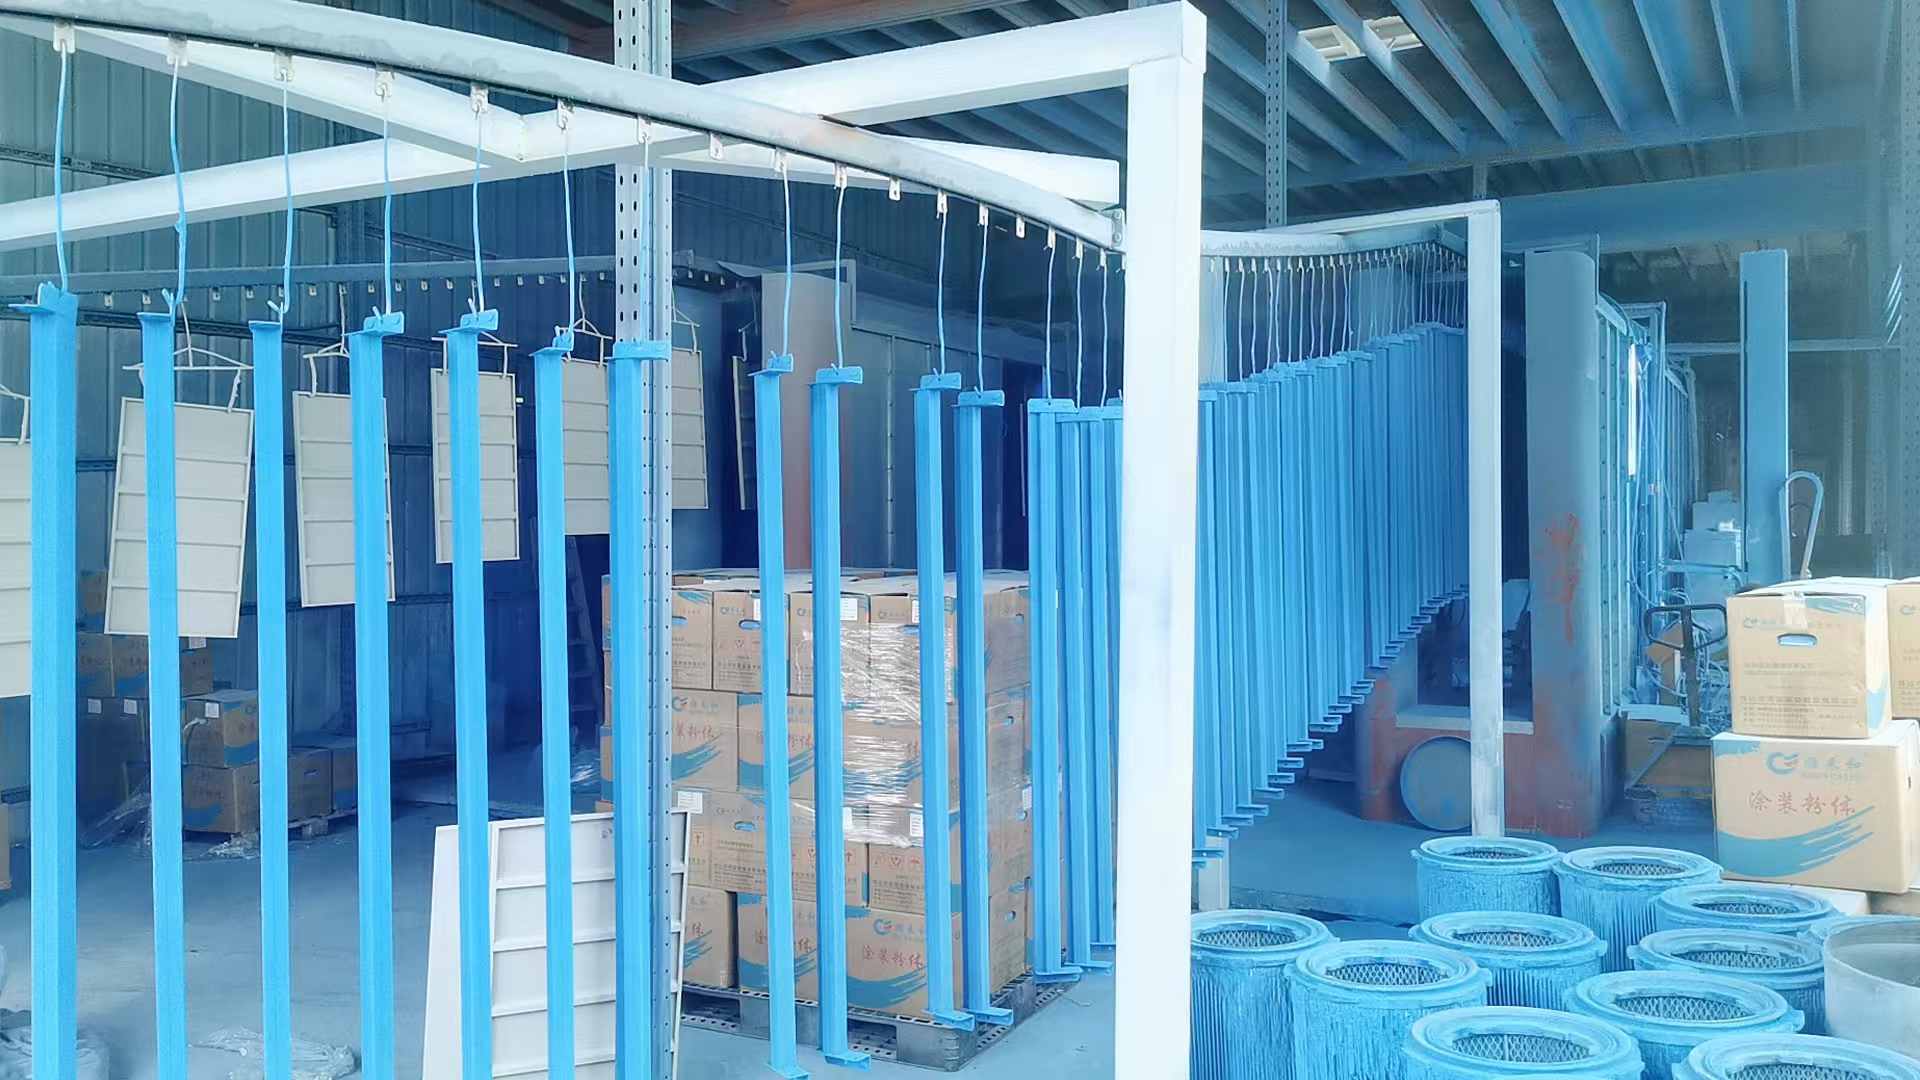
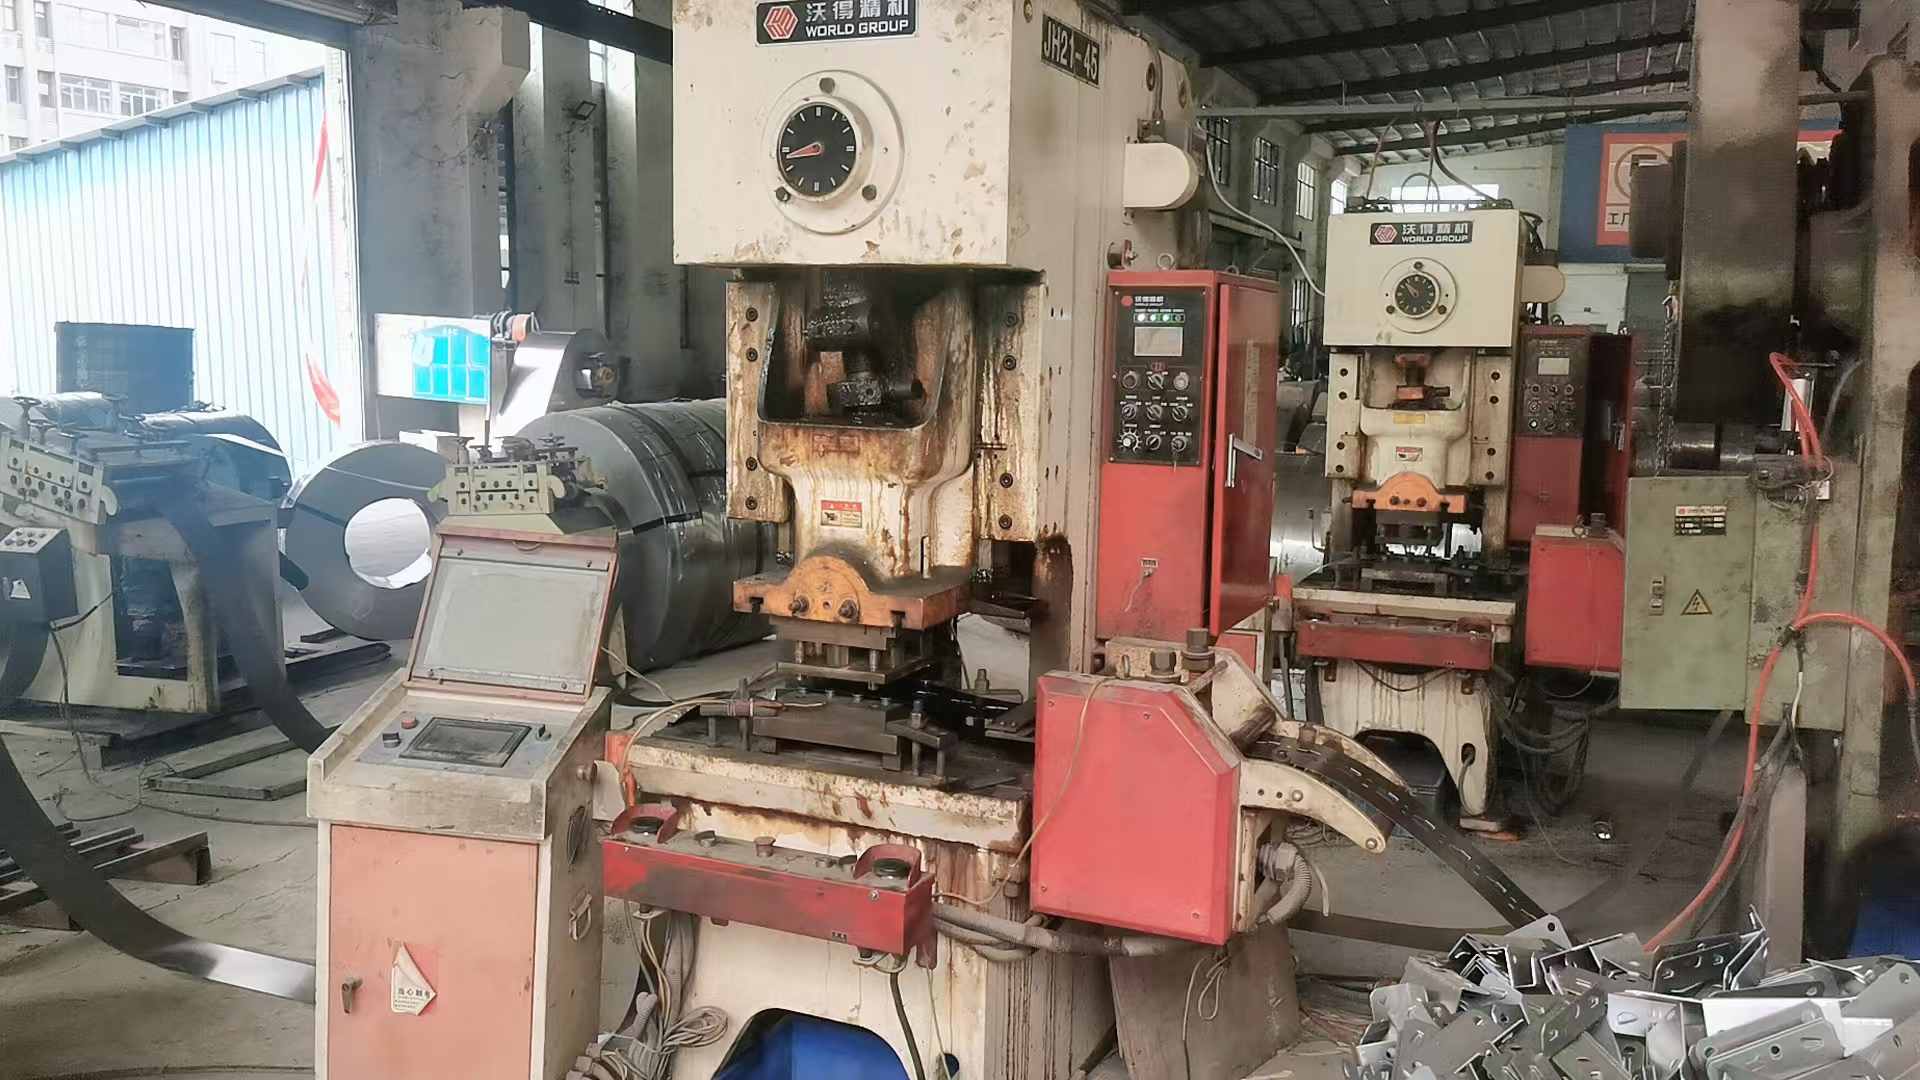
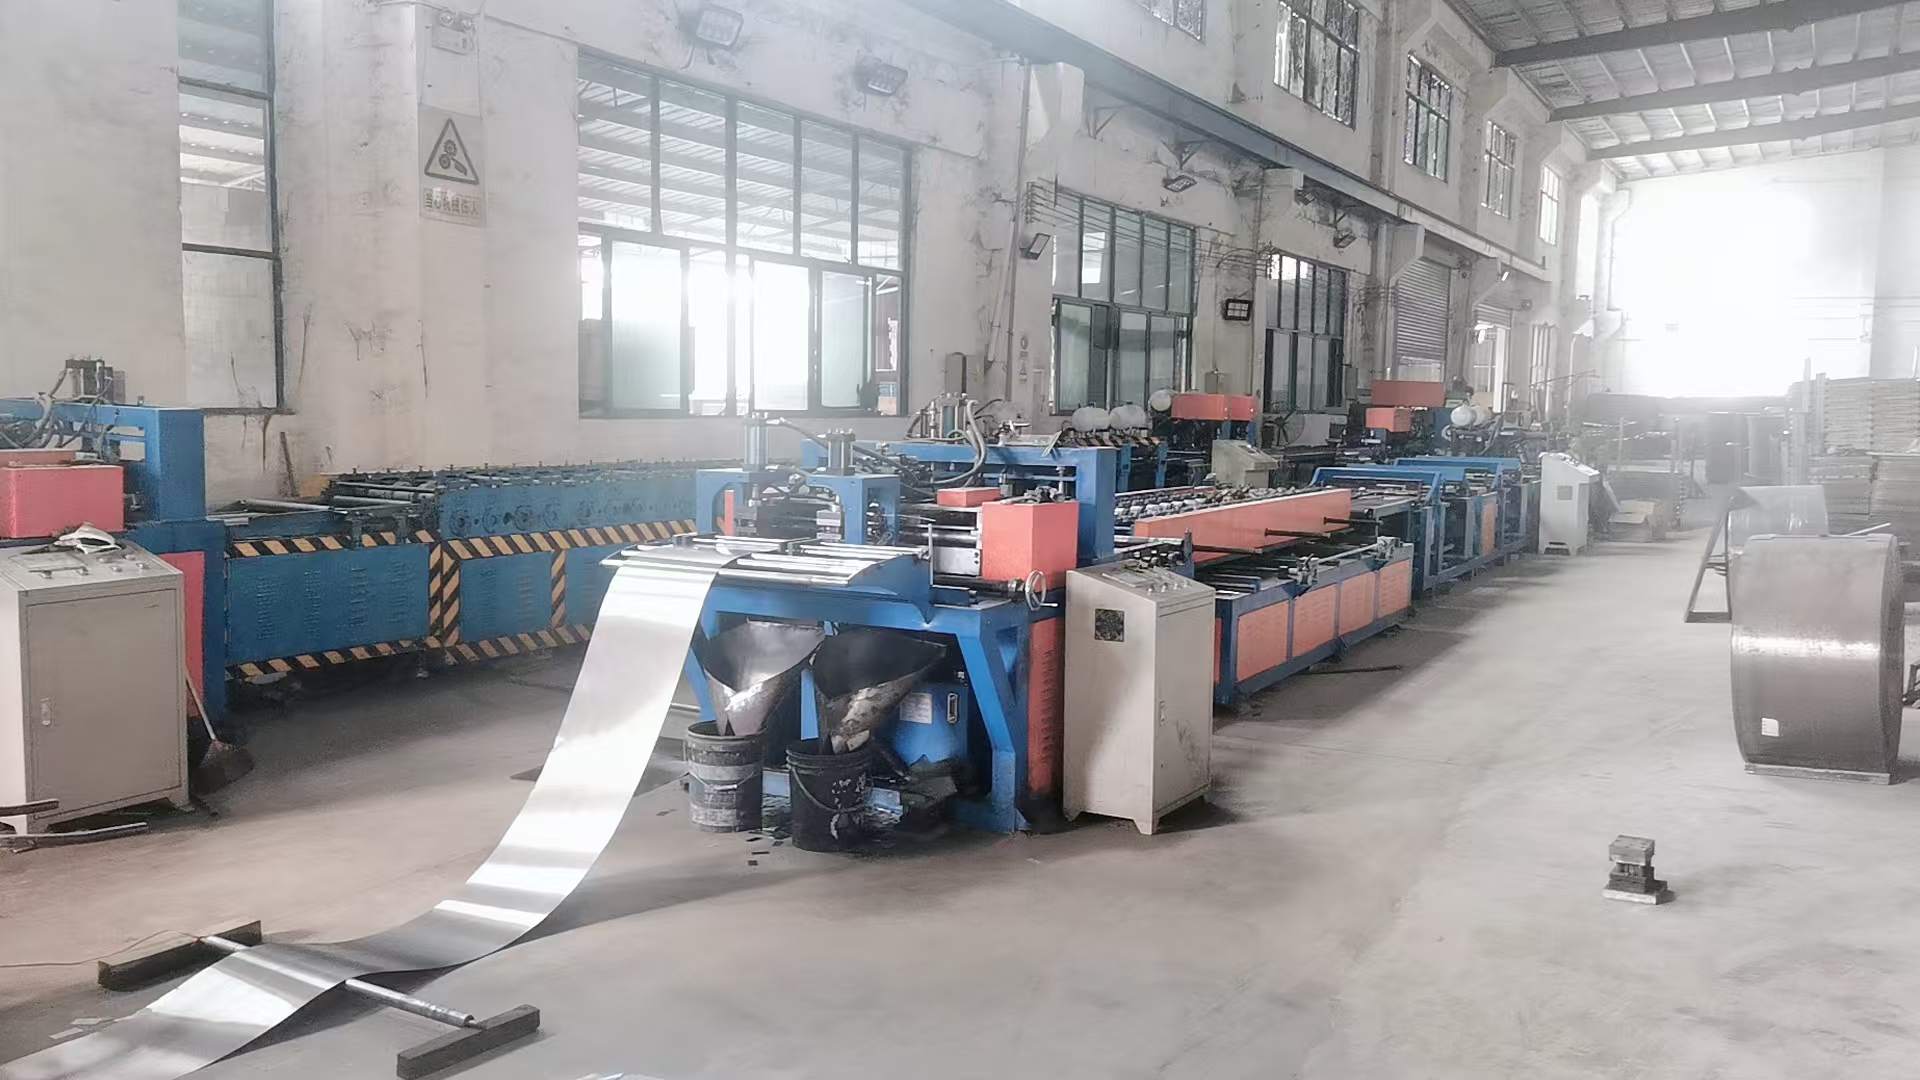
Our technology roadmap emphasizes advanced cold-rolled steel processing, automated laser roll forming, robotic MIG welding, and electrostatic powder coating. These innovations ensure that every pallet rack, cantilever system, and mezzanine floor complies with European safety standards, offering superior resistance against seismic activity, heavy dynamic loads, and environmental degradation in industrial environments.
Frequently Asked Questions (FAQ)
What certifications do your tool storage solutions and warehouse racks possess?
All our storage solutions, including heavy-duty pallet racks, cantilever systems, and mezzanine floors, are manufactured in strict accordance with international standards and carry CE certification. Our production facilities operate under ISO quality management systems, ensuring full structural integrity and compliance with global safety regulations.
Can you customize storage rack dimensions and load capacities for specific industrial requirements?
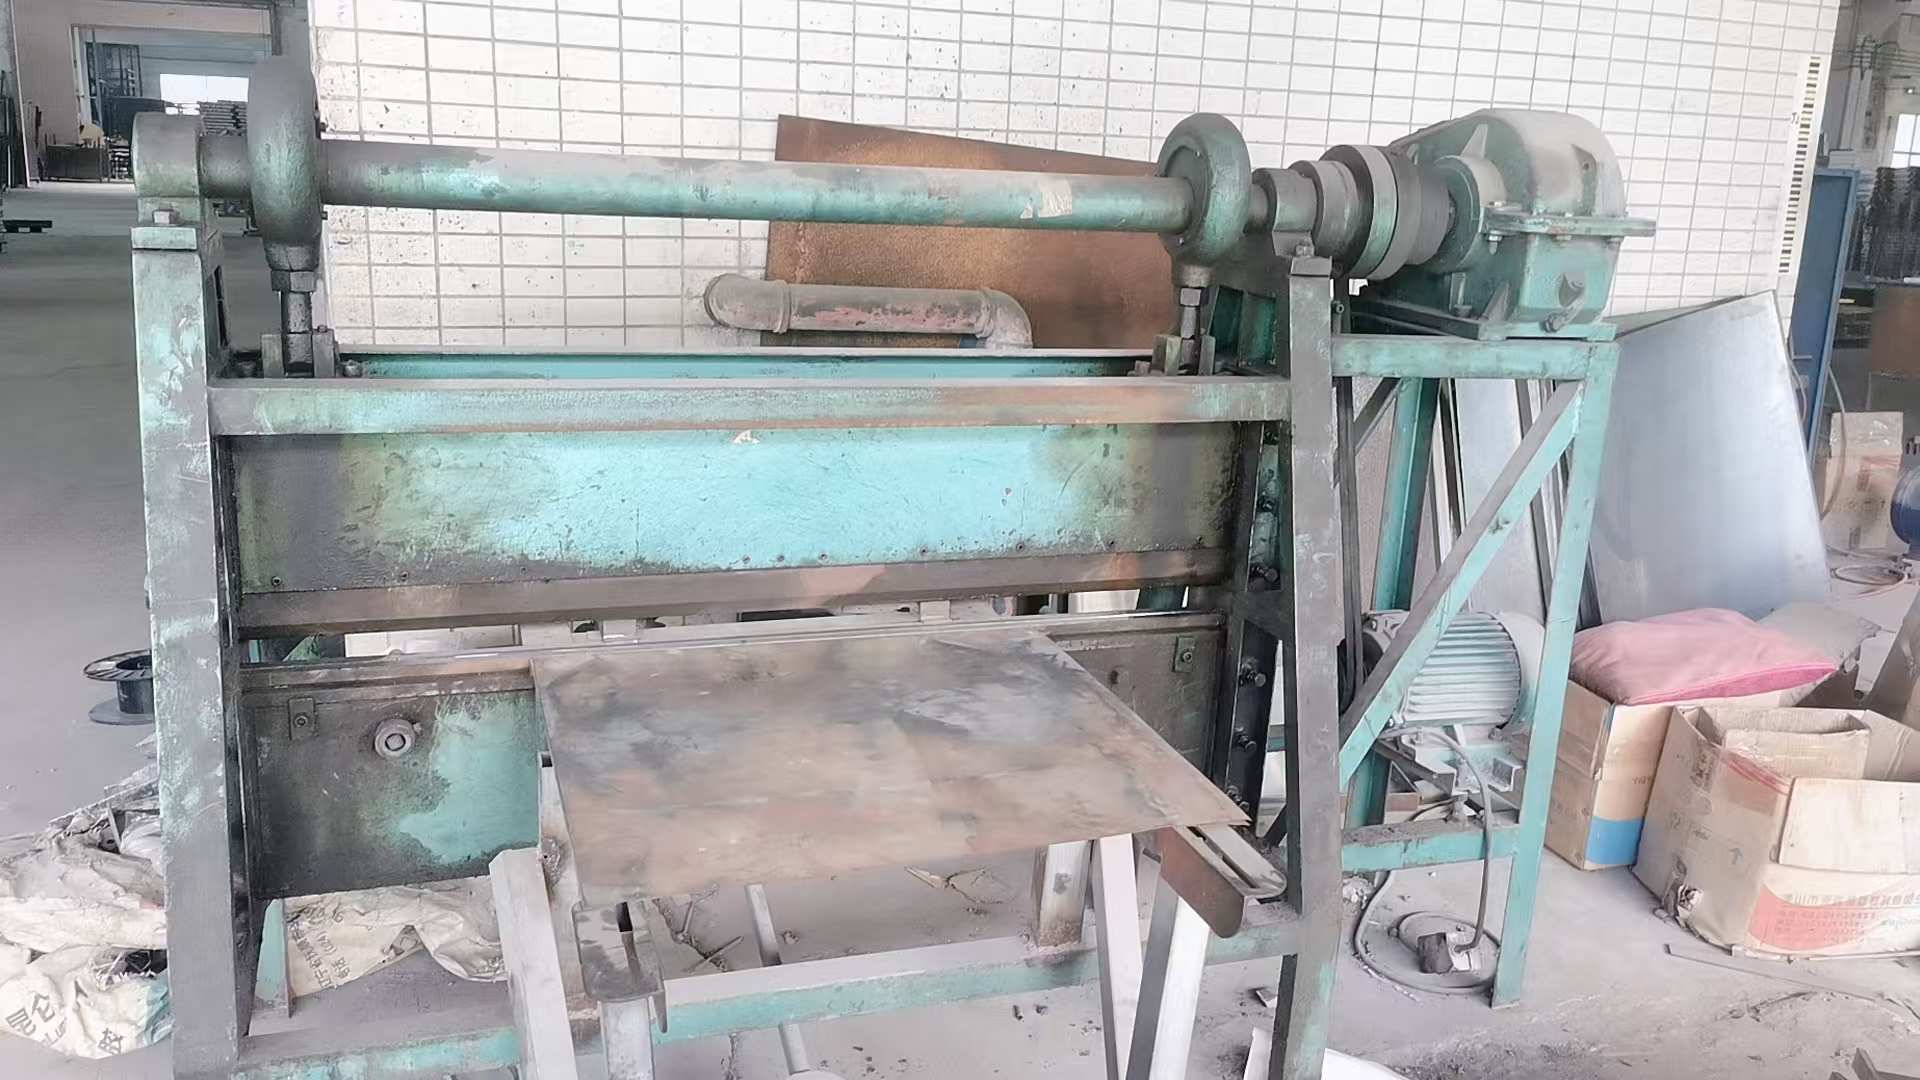
Yes. With our team of 126 professional R&D engineers and advanced manufacturing lines (such as laser roll forming and automated bending machines), we provide fully customized OEM/ODM services tailored to your exact warehouse layout, vertical clearance, and load-bearing demands.
What surface treatment processes are applied to prevent corrosion and wear?
We utilize automated electrostatic powder coating lines and specialized anti-rust treatments. Raw materials undergo rigorous surface cleaning, phosphating, and high-temperature curing to ensure superior adhesion, scratch resistance, and long-term durability in harsh workshop environments.
 Hui Lian